Palletizing Throughput: Estimating Capacity Without Confusing It with Robot Speed
Calculate palletizing capacity from picks, cycle time, pallet exchange and stated downtime assumptions, with a worked example and sensitivity table.
For a repetitive pallet sequence, estimate ideal capacity as 3,600 × cases per pallet ÷ seconds per pallet. The seconds must include every non-overlapping activity inside the cell boundary. Robot travel speed alone does not provide that time.
Then state how the ideal sequence relates to the scheduled period. If you apply a run-time factor, define its denominator and exclusions so that the same delay is not deducted twice.
Build a time budget
For identical picks, use:
T = P × t + e + s
Qideal = 3,600 × N ÷ T
| Symbol | Meaning | Unit |
|---|---|---|
| N | Cases completed on one pallet | Cases/pallet |
| P | Robot picks needed for that pallet | Picks/pallet |
| t | Complete average pick cycle: acquire, move, place and return | Seconds/pick |
| e | Non-overlapping pallet exchange time | Seconds/pallet |
| s | Other non-overlapping recurring time, such as sheet placement | Seconds/pallet |
| T | Total recurring time for one completed pallet | Seconds/pallet |
| Qideal | Output while this defined sequence repeats without extra loss | Cases/hour |
If pick times vary, sum the individual times instead of using one convenient fast cycle. If two tasks overlap, use the actual event sequence or a validated model; adding both full durations would overstate the elapsed time. Confirm the handling unit: MHI’s taxonomy distinguishes picking concepts from layer transfer, which is why a “cycle” needs an explicit definition.
Worked example: assumed inputs
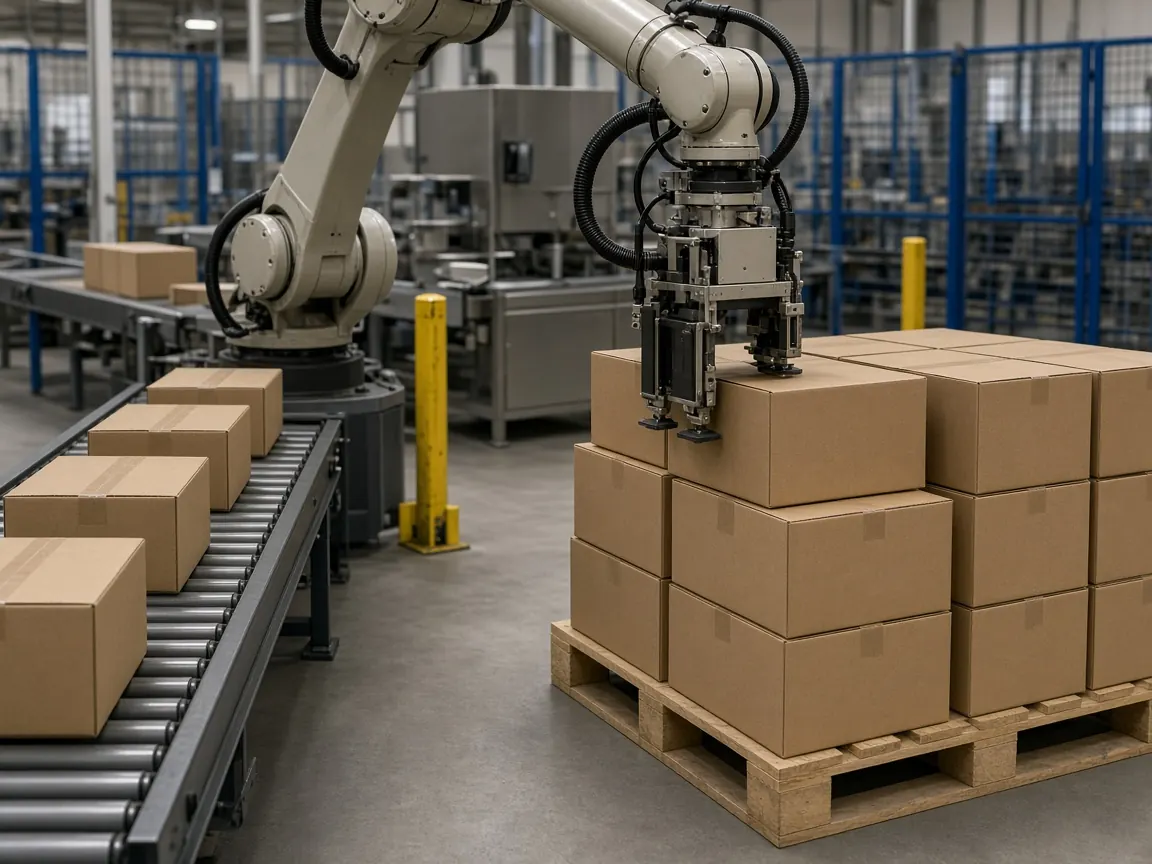
Assume 60 cases per pallet, two cases on every pick, an eight-second complete pick cycle, and 30 seconds of pallet exchange that cannot overlap robot work. Assume no sheet handling. These are invented planning inputs for arithmetic, not manufacturer specifications or a measured project.
- Picks per pallet:
60 ÷ 2 = 30. - Recurring time:
30 × 8 + 30 = 270 seconds. - Ideal output:
3,600 × 60 ÷ 270 = 800 cases/hour. - With an assumed 90% run-time factor:
800 × 0.90 = 720 cases/hourover the stated scheduled period.
Here the 90% factor covers additional lost time beyond the recurring sequence, such as interruptions not already included. It does not deduct pallet exchange again. We assume no rejected cases in this example; if rejected or reworked cases matter, define whether output counts all handled cases or only accepted cases.
Sensitivity: change one assumption
All rows retain 60 cases per pallet and the same assumed 90% run-time factor. Results are rounded to the nearest whole case per hour.
| Scenario | Recurring seconds/pallet | Scheduled-period cases/hour |
|---|---|---|
| Base: two cases/pick, eight seconds, 30-second exchange | 270 | 720 |
| Exchange takes 60 seconds | 300 | 648 |
| Complete pick cycle takes ten seconds | 330 | 589 |
| Only one case is handled per eight-second pick | 510 | 381 |
A change in group size may also change acquisition time or tooling. The last row isolates one variable to show sensitivity; it is not a prediction that a real single-case cell uses the same cycle.
Check the surrounding line
If upstream supplies fewer accepted cases than the cell can handle, the cell waits. If downstream cannot remove full pallets, accumulation eventually fills. A buffer can absorb a temporary mismatch; it cannot sustain a permanent excess arrival rate.
For example, an assumed arrival of 12 cases/minute against service of ten cases/minute for three minutes adds six cases to a queue, provided both rates hold and no other transfers intervene. Size and control a real buffer from arrival records and the complete sequence, not this example.
For the RFQ, provide product mix, cases per pallet, group sizes, observed arrival pattern, exchange method, shift calendar, and the exact definition of accepted output. The simulation guide helps evaluate interacting delays; the palletizing index covers the equipment decisions behind those inputs.
Sources and scope
Source dates refer to the material consulted, not independent performance verification.
- MHI: Unit Load Formation Equipment
Handling can occur by case/group or layer; the article calculation is an explicitly assumed editorial example
undated · Checked October 6, 2026
Published by DeltaSpark. Editorial policy · Corrections and contact
Continue reading
Robotic Palletizing Systems: Types, Components and Selection Criteria
Define a complete robotic palletizing cell, compare handling concepts, and collect the product, pallet and interface data needed for a proposal.
Read articleWhat Simulation Can and Cannot Tell You About a Palletizing System
Match palletizing simulation outputs to model inputs, assumptions and physical checks before using animations or capacity estimates in a project.
Read article
Palletization Meaning and Unit-Load Engineering: Footprint, Support and Stability
Palletization builds a unit load for handling and transport. Check footprint, package support, center of gravity and restraint before approving a pallet pattern.
Read article